Choosing a China Top Vision Laser Marking Machine Manufacturer requires more than comparing prices or browsing polished product photographs. A dependable supplier should demonstrate real manufacturing experience, stable optical performance, and practical knowledge of production lines. The machine must recognize each workpiece, locate its fiducial points, and place a clean mark despite small positioning differences. In a busy factory, that difference matters.
Theodore H. Maiman, a pioneer of laser technology, once said, “The laser is a solution looking for a problem.” His observation remains relevant today. A Vision Laser Marking Machine should solve a defined production problem, not become an impressive but unnecessary purchase. For example, a camera-guided fiber laser can identify irregular metal housings, correct their position, and engrave a readable QR code within seconds. UV systems may suit sensitive plastics, while CO₂ lasers often serve selected non-metallic materials.
Performance needs evidence. Ask manufacturers for sample marks, camera accuracy data, repeatability results, and long-term service records. Inspect the marking depth under actual lighting. Check whether software supports traceability, barcode verification, and easy recipe changes. Small details expose major weaknesses. A fast demo may hide unstable calibration or weak after-sales support.
No supplier is perfect. Even experienced manufacturers can overlook operator training, fixture design, or factory dust. That deserves reflection. The strongest evaluation combines technical testing, customer references, safety compliance, and transparent communication. This article examines the features, applications, quality indicators, and selection criteria that define a trustworthy Chinese Vision Laser Marking Machine manufacturer.
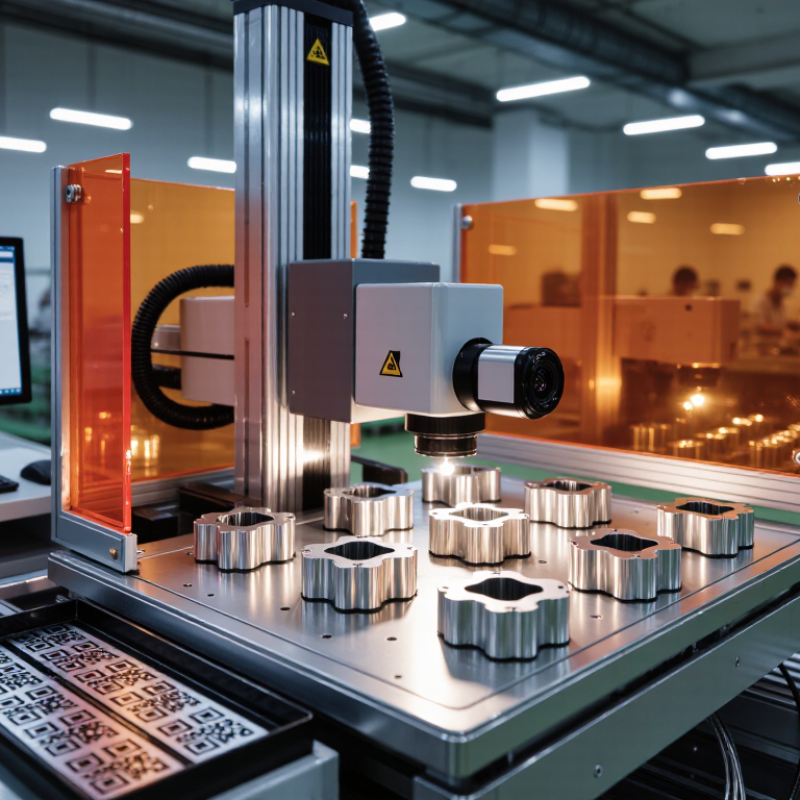
A vision laser marking machine combines a laser marker with an industrial camera. The camera identifies a part’s position, shape, or reference point. The laser then places text, codes, symbols, or patterns accurately. Unlike a standard marker, it can adjust marking paths when parts shift slightly.
Its main components include a laser source, scanning galvanometer, focusing lens, camera, lighting system, controller, and marking software. An enclosure and fume extraction system support safer operation. The camera needs stable lighting and a clear view. Poor contrast can cause incorrect recognition. This detail is often underestimated.
In practical production, operators use vision systems for serial numbers, batch information, alignment marks, and traceability codes. Common materials include metal, plastic, coated surfaces, and selected electronic components. Before regular production, technicians should test contrast, depth, speed, and readability. Calibration also requires attention. A small lens error may create visible position differences across the work area. Vision software is helpful, but it is not perfect. Reflective surfaces, dust, curved parts, or damaged samples can confuse the camera. Human inspection remains valuable for unusual results. Safety interlocks, ventilation, protective enclosures, and trained operation should match the laser class and local requirements.
In precision marking, the camera is not decoration. It acts as the machine’s measurement eye. A vision-guided system captures fiducial points on each workpiece. Software compares these points with programmed coordinates. It then corrects rotation, translation, and placement differences before the laser fires. Small errors become visible.
Achieving ±0.02 mm requires more than a sharp camera. Lens distortion must be calibrated with a certified reference grid. Lighting should reveal edges without glare, especially on polished metal or dark plastic. The controller converts camera pixels into laser coordinates. A rigid fixture also limits movement during marking. Under controlled conditions, this workflow can reach the stated positioning tolerance.
But not everywhere. Temperature changes, vibration, surface variation, and poor focus can quickly consume the tolerance. An experienced technician checks repeatability with reference samples, rather than trusting one successful mark. I have seen rushed calibration produce convincing results that fail after several hours. That is the uncomfortable lesson. Regular verification, clean optics, and measured fixture wear keep accuracy credible. Manufacturers should publish test conditions, sampling methods, and tolerance data. This transparency helps buyers judge performance realistically.
1064 nm
Choosing a laser wavelength is a material decision, not a prestige decision. In production trials, 1064 nm systems usually mark stainless steel, aluminum, brass, and many engineering plastics effectively. They create dark annealed marks, bright ablation, or shallow engraving. Aluminum can reflect energy, so pulse width and power need careful adjustment.
532 nm
Fast, but not universal. 532 nm green lasers offer stronger absorption on reflective metals, including copper and some precious-metal surfaces. They also suit sensitive plastics, glass, wafers, and miniature electronic parts. The smaller focused spot can improve contrast, although alignment becomes less forgiving.
A 2024 report from MarketsandMarkets identifies fiber-based marking as the leading technology segment, supported by ongoing metal-processing demand.
10.6 µm
At 10.6 µm, CO2 energy is strongly absorbed by wood, paper, cardboard, leather, acrylic, rubber, and many coated materials. It can produce crisp surface contrast without deep cutting. Bare metals usually respond poorly unless a suitable coating is applied.
Grand View Research’s 2024 industry analysis also reports continued growth in laser marking, driven by traceability across packaging and manufacturing.
These figures show market direction, not a guaranteed process result. I would test scrap material first. Surface finish, additives, moisture, and heat sensitivity can overturn a textbook choice.
China Top Vision Laser Marking Machine Manufacturer?
How to Assess Chinese Manufacturers Using ISO 9001 and IEC 60825-1
ISO 9001 is a useful starting point when assessing a Chinese laser marking machine manufacturer. The ISO Survey 2022 recorded more than 1.26 million ISO 9001 certificates worldwide. That figure shows its broad adoption, but certification alone proves little about machine quality. Request the certificate number, issuing body, scope, and expiry date. The scope should cover design, assembly, testing, or servicing of laser equipment, not only general trading.
IEC 60825-1 focuses on laser product safety. Ask for the declared laser class, accessible emission measurements, warning labels, interlocks, and enclosure test records. A reliable factory should explain these items clearly. Watch a live demonstration. The door should stop emission immediately, and the control panel should show a clear fault condition. Request risk assessments, electrical test reports, user manuals, and maintenance instructions. Do not accept copied documents without matching model numbers. Small inconsistencies matter.
Tips: Compare the certificate scope with the actual production floor. Check calibration dates on power meters. Ask for sample marking tests on your material, including speed, power, depth, and repeatability. ISO 9001 supports process control, while IEC 60825-1 supports laser safety. Neither guarantees perfect marking results. My own caution is simple: a polished audit file can still hide weak after-sales support. Speak with recent customers, inspect spare-parts procedures, and record every technical promise in the contract.
This screening chart uses a custom 100-point evidence rubric. ISO 9001 focuses on quality-management processes, while IEC 60825-1 focuses on laser-product safety classification, labeling, user information, and protective measures. The point allocation is an evaluation framework, not a claim about any specific company.
China Top Vision Laser Marking Machine Manufacturer?
What Production Data Matters: 20–100 kHz, 30–100 W, and System Uptime
A serious laser marking evaluation starts with production evidence, not catalogue speed. Pulse frequency between 20 and 100 kHz affects marking texture, contrast, and cycle stability. Power from 30 to 100 W supports different materials and line speeds, but higher wattage does not automatically improve output. On coated aluminum, for example, 50 W at 50 kHz may produce cleaner contrast than 100 W with excessive heat.
Measure the result on your parts.
ISO 22400 identifies availability, performance, and quality as core manufacturing metrics. The OEE Foundation’s benchmark guidance often places world-class OEE near 85%, while many factories remain close to 60%. For a marking cell, uptime includes more than laser firing. Record warm-up time, fixture changes, alarm recovery, lens cleaning, software delays, and rejected codes. A machine marking for eight hours can still lose hundreds of parts through small interruptions.
A practical acceptance test should log cycle time, first-pass yield, and unplanned stops across several shifts. Test 20, 50, and 100 kHz settings with 30, 50, and 100 W configurations. Keep the material, artwork, and fixture constant. Industry automation reports consistently emphasize traceability and equipment connectivity, yet manual downtime records are often incomplete. That weakness deserves attention. The fastest setting may also create more rejects, and my initial assumption may be wrong without production data.
Production-oriented reference data for evaluating industrial fiber laser marking systems
| Evaluation Dimension | Production Reference Range | Why It Matters | Recommended Verification Method | Production Interpretation |
|---|---|---|---|---|
| Laser Type | Q-switched pulsed fiber laser | Provides short pulses suitable for permanent marking on metals, coated materials, and selected engineering plastics. | Request the pulse profile, wavelength, beam quality data, and application samples. | Common industrial configuration for general-purpose marking and light engraving. |
| Output Power | 30–100 W | Higher power can increase throughput or support deeper engraving, but it does not automatically improve contrast or edge quality. | Measure power at the work plane with a calibrated power meter and compare it with the specified value. | 30 W is often adequate for standard marking; 50–100 W is more suitable for heavier production or deeper engraving. |
| Pulse Repetition Frequency | 20–100 kHz | Frequency influences pulse energy, heat input, contrast, surface finish, and marking behavior. | Confirm the usable frequency range at the selected power rather than checking only the maximum specification. | Lower frequencies generally provide higher pulse energy; higher frequencies can support smoother and faster surface marking. |
| Pulse Energy | Approximately 0.3–1.5 mJ | Pulse energy is determined by average power divided by pulse frequency and is important for engraving depth and material response. | Calculate energy from measured average power and verified pulse frequency; review the manufacturer’s pulse-energy curve. | A 30 W system at 20 kHz has a theoretical average pulse energy of about 1.5 mJ before optical losses. |
| Maximum Galvo Scanning Speed | Up to approximately 7,000–12,000 mm/s | Higher scanner speed can reduce cycle time, but actual output depends on hatch spacing, character size, acceleration, and laser settings. | Run a timed test using the real marking pattern, line spacing, font, and material. | Use actual cycle time—not the maximum scanner speed—as the main productivity metric. |
| Positioning Accuracy | Typically about ±0.01–0.03 mm in a properly calibrated system | Accuracy affects code placement, small characters, graphics, and repeatability between workpieces. | Verify with a calibrated grid, dimensional artifact, or vision-based measurement at multiple positions in the marking field. | Accuracy varies with lens field size, mechanics, calibration quality, temperature, and workpiece fixturing. |
| Standard Marking Field | Approximately 70 × 70 mm to 300 × 300 mm | The field size determines the maximum marking area and affects spot size, resolution, and working distance. | Confirm the actual lens model, focal length, field distortion, and usable edge performance. | Smaller fields generally provide finer detail; larger fields improve coverage but may reduce resolution. |
| Typical Marking Materials | Stainless steel, mild steel, aluminum, brass, copper, anodized aluminum, coated metals, selected plastics | Material composition and surface treatment strongly influence contrast, heat-affected area, and achievable depth. | Test production-grade samples, including the actual surface finish, coating, oil condition, and batch variation. | Material trials are essential because identical nominal materials can mark differently after treatment or machining. |
| Code Reading Performance | Target >99% first-pass readability after process validation | Readable 1D and 2D codes are more valuable than visual appearance alone in traceability applications. | Use the intended barcode verifier, lighting, camera, and quality grade standard on a representative production batch. | Define acceptance criteria for contrast, cell geometry, quiet zones, distortion, and permanence before purchase. |
| Cycle-Time Measurement | Record marking time, loading time, unloading time, and inspection time separately | Laser-on time is only one part of the total production cycle. | Measure at least 30 consecutive cycles under normal operator and material conditions. | Throughput should be reported as completed, accepted parts per hour rather than scanner speed alone. |
| System Availability Target | ≥95% planned production availability | Availability reflects the time a validated system is ready for scheduled production, excluding planned maintenance where defined. | Track scheduled production time, downtime events, fault duration, changeover time, and planned maintenance separately. | Use a written availability definition because supplier uptime figures may exclude setup, material changeovers, or operator delays. |
| Mean Time Between Failures | Monitor by subsystem; establish a site-specific baseline | Laser source, scanner, controller, exhaust, chiller, safety circuit, and motion equipment can have different failure patterns. | Request service records and calculate MTBF from logged production faults after installation. | A single system-level MTBF claim is less useful than transparent failure data by component. |
| Mean Time to Repair | Common target: under 2 hours for routine replaceable faults | Fast diagnosis and modular replacement reduce lost production time. | Check spare-parts availability, remote diagnostic capability, fault-code records, and technician response procedures. | Repair time depends on local support, access to parts, training, and the fault type. |
| Scheduled Maintenance | Routine cleaning and inspection: daily to monthly; frequency depends on environment and duty cycle | Dust, smoke, oil mist, lens contamination, and poor cooling conditions can reduce quality and uptime. | Review the maintenance schedule for optics, extraction filters, cooling, electrical connections, and safety devices. | Document cleaning intervals and assign responsibility before the machine enters production. |
| Cooling and Operating Environment | Typically clean, dry indoor operation; commonly around 5–35 °C for equipment, subject to system specifications | Temperature, humidity, dust, and condensation affect laser stability, electronics, optics, and marking consistency. | Confirm the permitted temperature, humidity, altitude, ingress protection, and required air-conditioning or extraction conditions. | Stable environmental control helps protect uptime and repeatability, especially in continuous production. |
| Safety and Compliance | Enclosed Class 1 system when properly integrated and interlocked | Enclosures, interlocks, emergency stops, warning indicators, and access controls help manage laser hazards. | Review the risk assessment, safety circuit validation, guarding, labeling, and applicable local requirements. | Safety status must be verified for the complete installed system, not only for the laser source. |
| Data and Integration | USB/Ethernet or industrial I/O; optional PLC, MES, scanner, and vision integration | Reliable data exchange reduces manual entry errors and supports traceability. | Test recipe selection, serial-number handling, duplicate-code prevention, job permissions, and production-data logging. | Integration quality can affect effective throughput as much as the laser’s optical performance. |
| Acceptance-Test Priority | Sample quality, cycle time, readability, repeatability, safety, and uptime readiness | A structured acceptance test converts specifications into measurable production outcomes. | Use signed test criteria with approved materials, approved artwork, target cycle time, and defined defect limits. | Purchase decisions should be based on verified production results rather than headline specifications. |
Data note: The figures are general industrial reference ranges for evaluating pulsed fiber laser marking systems. Actual results depend on laser architecture, optics, scan field, material, artwork, fixturing, environmental conditions, software settings, and maintenance practices. Uptime values are production targets or measurement frameworks, not guaranteed performance.
A camera captures fiducial points on each workpiece. Software compares them with programmed coordinates. It corrects rotation, position, and translation before marking. Small errors become visible.
No. This tolerance requires controlled conditions. Calibration, stable temperature, rigid fixtures, and proper focus matter. Vibration or surface variation can quickly consume the tolerance. One successful mark proves very little.
Use a certified reference grid. Check lens distortion and pixel-to-laser conversion. Verify repeatability with several reference samples. A rushed calibration may look convincing at first.
Lighting should reveal edges without glare. Polished metal often needs carefully angled illumination. Dark plastic may require stronger, more even light. Poor lighting creates false edges.
Request certificate details, safety records, manuals, and maintenance instructions. Check the certificate scope, issuer, number, and expiry date. Model numbers should match every document. Small inconsistencies matter.
Confirm the declared laser class and enclosure test records. Check warning labels, interlocks, and accessible emission measurements. Open the door during a live demonstration. Emission should stop immediately.
Record cycle time, first-pass yield, warm-up time, and rejected parts. Track fixture changes, alarms, cleaning, and software delays. Test 20, 50, and 100 kHz settings. Compare 30, 50, and 100 W configurations.
Not necessarily. Higher power can create excessive heat or more rejects. For coated aluminum, moderate power may produce cleaner contrast. The fastest setting may not be the most productive. I would not trust assumptions without shift-based data.
A Vision Laser Marking Machine combines a laser source, optical scanning system, industrial camera, motion platform, control software, and safety enclosure to identify product features and place marks accurately. Its vision guidance system captures the workpiece position, compares it with a programmed reference, and automatically adjusts the marking path, helping achieve positioning accuracy of approximately ±0.02 mm. This makes the equipment suitable for electronics, automotive parts, medical devices, packaging, and other applications requiring traceable, durable identification.
Selecting the correct wavelength is essential: 1064 nm commonly suits metals and many engineering plastics, 532 nm is useful for sensitive or reflective materials, and 10.6 µm is often selected for wood, glass, paper, and other organic surfaces. When evaluating Chinese manufacturers, buyers should review ISO 9001 quality processes, IEC 60825-1 laser safety compliance, component stability, service capability, and testing records. Key production data includes operating frequencies of 20–100 kHz, laser power from 30–100 W, marking speed, repeatability, and long-term system uptime.